 Surgical · Dental · Precision Instruments Surgical · Dental · Precision Instruments
Precision-machined German & Japanese stainless steel instruments engineered for high-durability surgical performance and compliance with ISO 13485:2016 standard protocols.
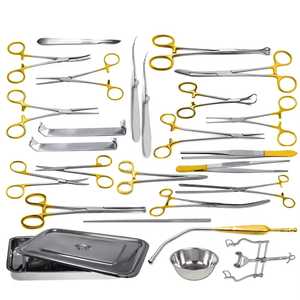
The global oral surgery landscape is undergoing a rapid paradigm shift toward minimally invasive tooth extraction (MIE) and immediate implant placement protocols. Within this clinical environment, the humble dental elevator has evolved into an instrument of micro-mechanical precision. Procurement directors, dental depot buyers, and hospital supply chain managers face mounting pressure to source high-grade, biocompatible, and fracture-resistant dental elevators that conform strictly to international regulatory frameworks (EU MDR 2017/745, US FDA 21 CFR 880, and ISO 13485:2016).
As premier China wholesale dental elevators suppliers and global exporters, our manufacturing ecosystem combines state-of-the-art CNC machining, hot die forging, vacuum heat treatment, and hand-honed blade dressing. This technical whitepaper explores the metallurgical science, mechanical ergonomics, regulatory compliance, and procurement trends shaping the future of dental extraction instruments worldwide.
The mechanical longevity and tactile feedback of a dental elevator are fundamentally governed by its alloy composition and thermal processing. Surgical grade stainless steel must balance high tensile strength, resistance to stress corrosion cracking (SCC), and edge retention after repeated steam sterilization cycles at 134°C.
We utilize specialized martensitic stainless steels—primarily AISI 420 (X20Cr13), AISI 440A, and custom German grade DIN 1.4116—for the working tips and functional shanks of dental elevators. Martensitic alloys contain high carbon content (0.15% to 0.75%) alongside 12% to 14% chromium, permitting deep heat-treatment hardening.
Conversely, for the ergonomic hollow handles, non-working sleeves, and color-coded identification rings, we implement austenitic stainless steel AISI 304 (X5CrNi18-10) or ultra-lightweight anodized titanium alloys. This multi-alloy construction reduces total tool mass while concentrating mechanical mass density at the functional working end.
Hardening in computer-controlled vacuum furnaces prevents surface decarburization, ensuring consistent 52–56 HRC hardness across every batch.
Compliant with ASTM A967 protocols, building a stable, corrosion-resistant chromium oxide passive layer over the entire metal surface.
Deep sub-zero cooling transforms retained austenite into tempered martensite, enhancing structural toughness and preventing tip deformation under torque.
Dental extraction requires converting rotational torque and linear push forces into gentle periodontal membrane detachment. As experienced China exporters, our catalog spans over 300 elevator variations grouped into four distinct functional classes:
Designed with straight shanks and concave blade faces, these instruments act as first-class levers. The fulcrum rests on the alveolar bone crest, allowing clinicians to expand the tooth socket gently. Our manufacturing protocol ensures the concave radius matches standard root curvature profiles.
Utilizing triangular or flag-shaped lateral working tips, these instruments convert hand rotation along the shank axis into powerful directional lifting forces. They are indispensable for removing fractured lower molar roots or retained root fragments.
Engineered with ultra-fine, tapered needle points (blade width < 1.8 mm), these tools allow precise navigation into deep apical thirds without destroying delicate interdental septa.
Luxating elevators feature razor-thin side bevels that cut PDL fibers axially rather than elevating via heavy torque. This prevents socket wall fractures and preserves labial bone plate integrity for immediate dental implant socket restoration.
| Elevator Category | Primary Clinical Mechanical Action | Blade Geometry Range | Hardness Spec (HRC) | Recommended Sterilization |
|---|---|---|---|---|
| Bein Straight Elevator | Wedge & First-Class Lever | 2.0 mm – 4.5 mm Concave | 54 – 56 HRC | Autoclave 134°C / 20 Mins |
| Cryer Triangular Elevator | Wheel-and-Axle Rotation | Left / Right Paired Blades | 53 – 55 HRC | Autoclave 134°C / 20 Mins |
| Heidbrink Root Tip Pick | Axial Micro-Wedging | 1.2 mm – 1.8 mm Tapered | 52 – 54 HRC | Autoclave 134°C / 20 Mins |
| Luxating Periotome | PDL Fiber Severing / Cut | 1.5 mm Ultra-Thin Flat/Curved | 55 – 57 HRC | Autoclave 134°C / 20 Mins |
| Coupland Elevator | Heavy Gouge Wedging | Sizes 1, 2, 3 (Gouge profile) | 54 – 56 HRC | Autoclave 134°C / 20 Mins |
As large-scale medical distributors and purchasing groups evaluate foreign manufacturing partnerships, several key industry trends dictate future inventory requirements:
Demand for golden TiN or DLC (Diamond-Like Carbon) nano-coatings is surging. These coatings increase surface hardness beyond 70 HRC, reduce tissue friction, and enhance visual contrast inside dark oral cavities.
Clinicians are shifting away from heavy solid handles toward hollow-core, large-diameter octagonal or textured silicone grip handles that minimize practitioner hand fatigue during long surgical sessions.
With EUDAMED and FDA UDI mandates fully enforced, every export unit requires direct laser etching of 2D Data Matrix codes for seamless hospital CSSD sterilization tracking.
Sourcing directly from a certified China dental instrument manufacturer provides global brands with an optimal balance of cost efficiency, engineering customization, and strict quality assurance.
Every dental elevator produced in our facility follows a standardized manufacturing route to eliminate batch-to-batch variance:
1. Material Inspection & Blanking: Certified raw steel bars undergo spectrographic analysis upon delivery. Mill test certificates are logged per LOT.
2. Hot Die Forging: Grain structures are aligned under heavy forging presses to establish structural density along the stress-bearing shank curvature.
3. 5-Axis CNC Milling: Box joints, screw threads, bevel angles, and serrations are machined within micrometer tolerances.
4. Hand Assembly & Alignment: Experienced technicians perform tip alignment, spring tension adjustment, and handle fitting.
5. Vacuum Hardening & Cryo Stabilization: Thermally treated to reach exact target hardness without surface scaling.
6. Precision Grinding & Surface Finishing: Satin, mirror, or matte black PVD finishes are applied, followed by edge honing.
7. Electrochemical Passivation: Ultrasonic bath cleaning followed by citric passivation to remove free iron particles.
8. Laser Marking & Final AQL Inspection: UDI markings, catalogue references, and brand logos are fiber-laser etched prior to sterile blister packing.
Here are direct technical and commercial answers to common questions received by our global export department:
Streamline your medical instrument sourcing with direct manufacturer pricing, ISO 13485 certified quality control, fast OEM turnaround, and global shipment support.
Send an Inquiry